Flip-Top vs. Screw Caps for Cosmetic Tubes: Hinge, Torque and Seal Selection
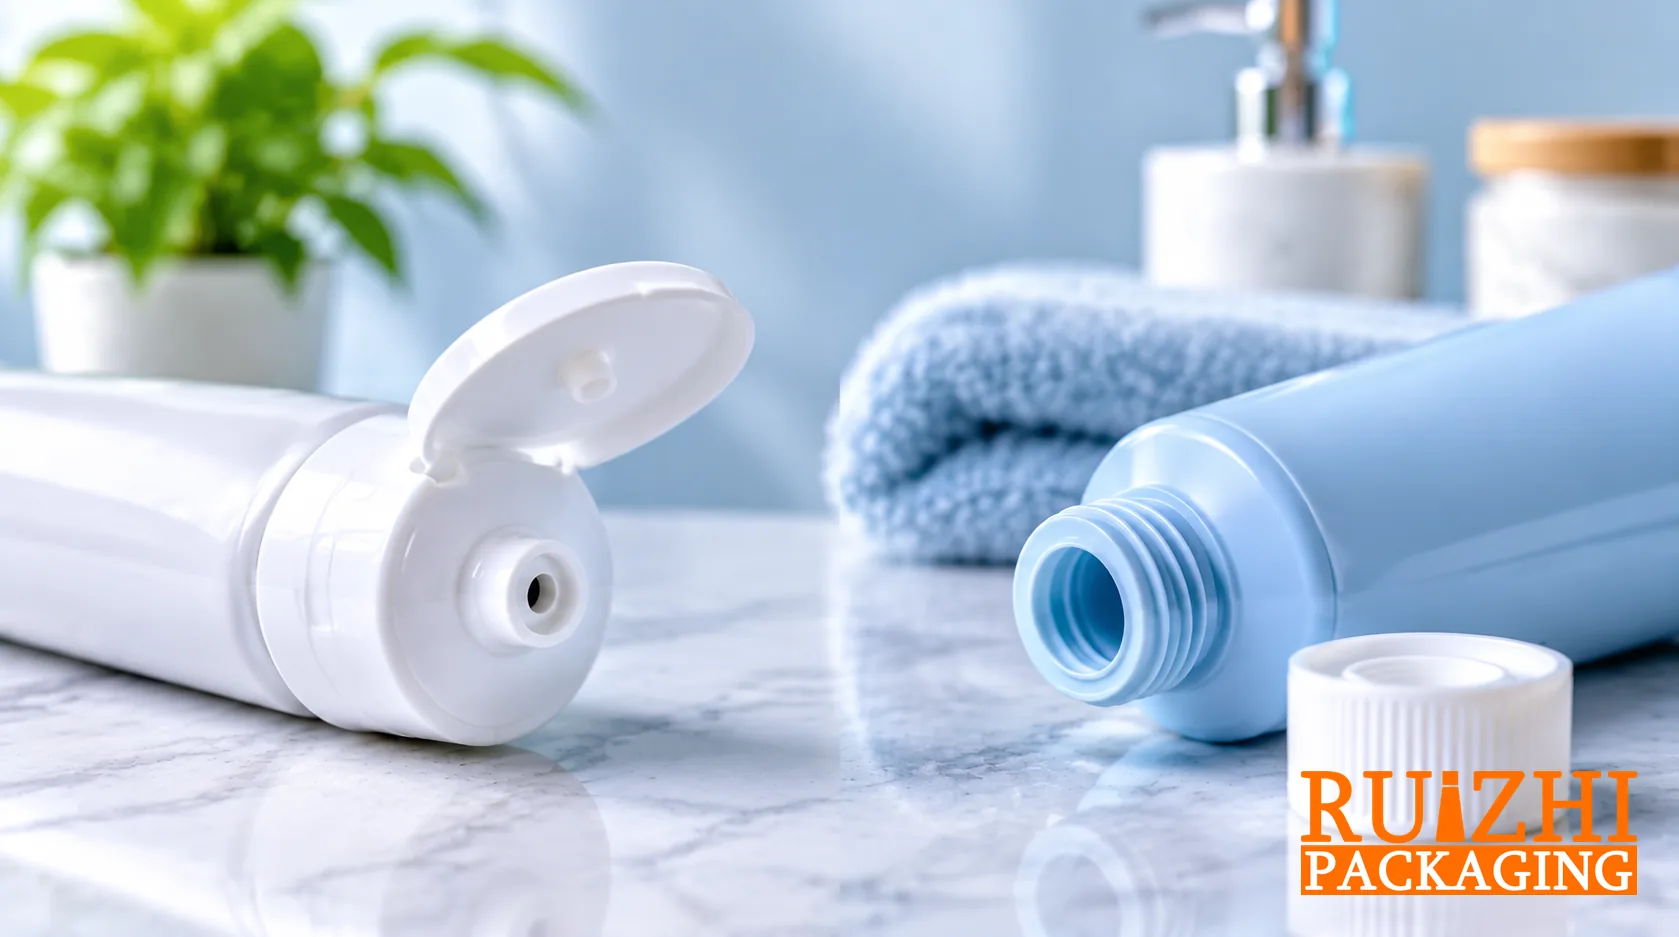
A cap is a functional part of cosmetic tubes packaging, not a finishing touch added after the tube is selected. Flip-top and screw caps create different opening routines, sealing interfaces and manufacturing controls. Choosing between them requires the formula, customer grip and filling process to be considered together. Neither style guarantees a leakproof pack simply because the sample closes with a satisfying click.
Map how customers open and store the product
A flip-top can be convenient for frequent one-handed use, especially when users dispense with the other hand. A screw cap can be familiar and may offer a clear threaded engagement. Yet a small cap can be hard to turn with wet fingers, and a hinge can collect formula. Observe actual users opening, dispensing and reclosing the pack rather than choosing from a catalog photograph.
Define what the seal actually is
The closure may seal at a plug, land, liner, or another interface. Ask for a section drawing and identify the dimensions that control contact. Threads provide retention but do not alone prove sealing. Test the assembled cap with the actual formula and inspect migration into threads or hinge cavities.
Specify torque and opening force
For screw caps, establish the application method, torque window or other agreed control, and a way to verify it on the line. Excessive tightening can make customers struggle or damage features; insufficient engagement can leak. For flip tops, measure opening force and inspect hinge return. The required limits should reflect product use and manufacturing capability, not an assumed universal value.
- Check closures after repeated cycling.
- Test upright, sideways and inverted storage.
- Evaluate residues around plugs, hinges and threads.
- Review accidental opening during distribution.
Match cap behavior to product flow
A thin lotion may seep where a thick cream does not. Product drying around the outlet can also change how a plug seats. Conduct dwell tests and assess first dispensing after storage. If users carry the pack in a bag, compression and temperature need consideration. A cap that passes a fresh-sample inversion check may still be unsuitable after repeated use.
Consider line and service requirements
Confirm cap feeding orientation, assembly speed and whether the filler applies caps manually or automatically. A decorative outer shell can complicate handling. Check that replacement components and color variants do not introduce uncontrolled changes in fit. Record the approved component and cavity or supplier references where available.
Make material and decoration decisions explicit
Cap resins, colorants and coatings need evaluation alongside the tube. Formula residue can attack a coating or make a smooth decorative cap slippery. Test on assembled packs after contact and use cycles. Avoid assuming that the same visual finish behaves identically on different substrates.
A strong closure brief records the seal concept, opening experience, retention, relevant test sequence and change controls. That makes the choice between flip-top and screw caps an engineering decision grounded in the customer's routine, not a generic preference for one style.
A development detail worth checking
Inspect multiple cap cavities or production lots where practical. A single excellent fit can hide dimensional variation across commercial output. Compare opening behavior after storage as well as immediately after assembly, because material relaxation can change the result. Keep the tube neck reference attached to the report so future buyers do not reuse closure approval on a different shoulder. ## Procurement review: turn the technical choice into a controlled order
For flip-top and screw cap closures, procurement should ask for a written specification rather than approve a photograph or a material name. Identify the finished formula reference, component drawing revisions, decoration standard and intended filling route. Classify requirements by their consequences: a cosmetic shade difference, a dispensing inconsistency and a leak require different investigation methods. Have the brand, packaging supplier and filling partner agree which characteristics are critical before requesting a commercial production release.
Sample evidence and acceptance limits
Select production-representative samples, including the intended resin, finish, assembly and decoration. Record component lot numbers and the conditions used for evaluation. A development sample made by a different process can answer an appearance question while leaving the manufacturing question unresolved. Ask the supplier to explain those differences explicitly. Retain signed samples as references, but support them with dimensions and measurable requirements because a physical reference alone cannot describe all functional limits.
Build the test plan around the failure modes described in this article. State sample conditioning, orientations, observation periods and acceptance rules before testing begins. Where measurements are necessary, specify the equipment and method. Results from different laboratories are difficult to compare when methods differ. A report saying only pass should prompt a request for underlying observations. Batch inspection sampling also serves a different purpose from compatibility or shelf-life work; one cannot replace the other simply because all use samples.
Quotation, pilot and change control
Compare quotations on total usable packs delivered to the filling location. Separate tooling, decoration setup, component costs, assembly, protective packing and transport assumptions. Clarify minimum quantities at component and color level, not just the total order. Include development samples, filling trials and expected start-up consumption in the purchasing plan. A cheaper pack can cost more overall if it requires extensive sorting, frequent line adjustment or avoidable disposal of filled rejects.
Run a pilot with the actual bulk and intended filling equipment before scaling up. Record interruptions, adjustments and reject causes. Resolve the findings with the supplier, then issue an approved production specification. Establish who owns tooling, how it is maintained and how artwork versions are controlled. Require notification when materials, finishes, factories or component sub-suppliers change. Even a visually similar substitute can affect performance, so approval of one version should not silently authorize every later variation.
Questions to settle before the purchase order
- Which production samples demonstrate the risks discussed here have been evaluated?
- What specification will the supplier and filler use for release?
- Which changes require written approval before shipment?
- Who investigates an assembled or filled-pack failure, and what evidence is retained?
These questions make a sourcing comparison more useful without assuming every supplier offers every construction. Confirm options for the specific design and order. Keep material descriptions, recycling claims and market requirements separate: a material may be available yet unsuitable for the formula, and technical suitability does not automatically substantiate a sustainability claim. Use the resulting evidence to choose a pack for its actual job, then preserve that evidence for repeat orders and future reformulations.
Explore related packaging
Compare the related collection , browse all packaging designs , review our OEM/ODM process , or send a project brief . Confirm the availability and specification of each option with our team before ordering.