Lip Gloss Tubes: Matching the Wiper, Wand and Container to Your Formula
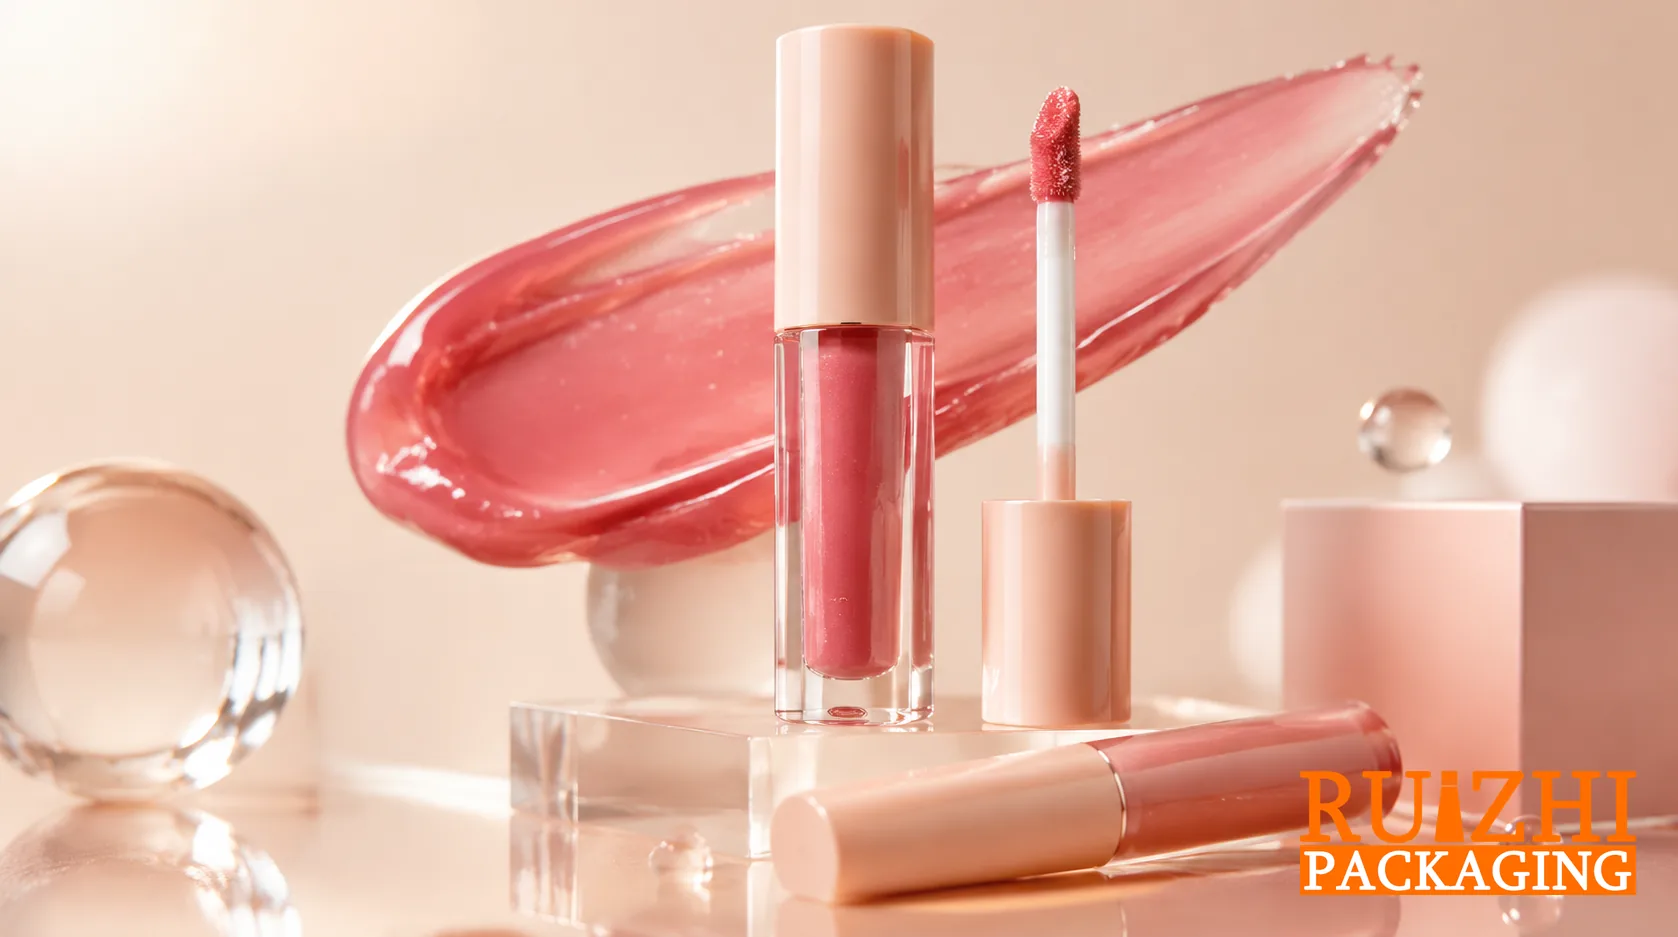
Lip gloss tubes succeed when the container, wiper, rod and applicator behave as one system. A transparent body and elegant cap may attract attention, but customers judge how much product the wand carries and whether the neck stays clean. Lip oil, pigmented gloss and liquid lip color can require different assemblies despite sharing the same nominal capacity and exterior silhouette.
Define pickup and application before choosing a wand
Ask how much product should remain on the applicator after withdrawal. A large flocked tip may hold substantial product, while a narrower shape can favor detail. The best shape depends on formula flow, pigment load and application technique. Compare realistic filled packs, not dry applicators displayed beside an empty bottle.
The wiper controls more than excess product
Wiper opening, flexibility and seating affect pickup, withdrawal force and leakage around the neck. A tight wiper may strip too much gloss or make withdrawal unpleasant. A loose one may overload the tip or allow product into the cap. Test the tolerance stack across production-representative parts rather than tuning one hand-assembled sample.
Evaluate the neck and closure as sealing interfaces
Confirm which surfaces form the seal when the cap is tightened. Product in threads can change closing behavior and create visible mess without a crack in the body. Check rod alignment, cap engagement and wiper retention after repeated use. Inspect filled packs upright, horizontal and inverted, including after temperature conditioning.
Low-viscosity lip oils deserve particular attention because they can travel through pathways that a thick gloss does not reveal. A pack sold for lip gloss should not automatically be approved for every oil-based formula. The final composition, finish and component materials all remain relevant.
Protect transparency and surface appearance
Clear bodies make discoloration, stress whitening and formula deposits visible. Review compatibility with the actual container material and any internal coatings. Ask whether external plating or decoration can contact leaked bulk during use. Fragrance and oils may also affect adhesives or decorative layers even when the body itself remains unchanged.
- Inspect wiper seating before and after cycling.
- Record applicator pickup using a repeatable procedure.
- Check residue around the neck and rod.
- Review cap finish after formula contamination.
Resolve filling and usable capacity
Nominal volume does not necessarily equal the approved fill. The rod and applicator displace space, and the filler needs headspace to insert the assembly cleanly. Confirm fill mass with actual bulk density and assembly sequence. Overfilling can create pressure and mess during closure installation, making a line problem look like a container defect.
Manage applicator changes as technical changes
A replacement flocking, wiper material or rod length can alter dose and fit. Record component references and ownership of approval. For repeat orders, require notification of substitutions rather than allowing visually similar parts to enter production without review. The application experience is part of the product specification and deserves the same control as color and logo placement.
A development detail worth checking
For a lip oil launch, keep the selected wand submerged for the intended conditioning period and examine the complete tip, rod and wiper. Record any swelling, loose fibers or changes in withdrawal. Evaluate how much product remains on the outside of the cap after normal use. This helps distinguish an application-load issue from leakage through the sealing interface. ## Procurement review: turn the technical choice into a controlled order
For lip gloss and lip oil tube assemblies, procurement should ask for a written specification rather than approve a photograph or a material name. Identify the finished formula reference, component drawing revisions, decoration standard and intended filling route. Classify requirements by their consequences: a cosmetic shade difference, a dispensing inconsistency and a leak require different investigation methods. Have the brand, packaging supplier and filling partner agree which characteristics are critical before requesting a commercial production release.
Sample evidence and acceptance limits
Select production-representative samples, including the intended resin, finish, assembly and decoration. Record component lot numbers and the conditions used for evaluation. A development sample made by a different process can answer an appearance question while leaving the manufacturing question unresolved. Ask the supplier to explain those differences explicitly. Retain signed samples as references, but support them with dimensions and measurable requirements because a physical reference alone cannot describe all functional limits.
Build the test plan around the failure modes described in this article. State sample conditioning, orientations, observation periods and acceptance rules before testing begins. Where measurements are necessary, specify the equipment and method. Results from different laboratories are difficult to compare when methods differ. A report saying only pass should prompt a request for underlying observations. Batch inspection sampling also serves a different purpose from compatibility or shelf-life work; one cannot replace the other simply because all use samples.
Quotation, pilot and change control
Compare quotations on total usable packs delivered to the filling location. Separate tooling, decoration setup, component costs, assembly, protective packing and transport assumptions. Clarify minimum quantities at component and color level, not just the total order. Include development samples, filling trials and expected start-up consumption in the purchasing plan. A cheaper pack can cost more overall if it requires extensive sorting, frequent line adjustment or avoidable disposal of filled rejects.
Run a pilot with the actual bulk and intended filling equipment before scaling up. Record interruptions, adjustments and reject causes. Resolve the findings with the supplier, then issue an approved production specification. Establish who owns tooling, how it is maintained and how artwork versions are controlled. Require notification when materials, finishes, factories or component sub-suppliers change. Even a visually similar substitute can affect performance, so approval of one version should not silently authorize every later variation.
Questions to settle before the purchase order
- Which production samples demonstrate the risks discussed here have been evaluated?
- What specification will the supplier and filler use for release?
- Which changes require written approval before shipment?
- Who investigates an assembled or filled-pack failure, and what evidence is retained?
These questions make a sourcing comparison more useful without assuming every supplier offers every construction. Confirm options for the specific design and order. Keep material descriptions, recycling claims and market requirements separate: a material may be available yet unsuitable for the formula, and technical suitability does not automatically substantiate a sustainability claim. Use the resulting evidence to choose a pack for its actual job, then preserve that evidence for repeat orders and future reformulations.
Explore related packaging
Compare the related collection , browse all packaging designs , review our OEM/ODM process , or send a project brief . Confirm the availability and specification of each option with our team before ordering.